|
Freezer environments present challenges that conventional pallet conveyor equipment simply isn't designed to handle. At temperatures as low as -20°F, mechanical components, lubricants, motors, sensors, and lifting mechanisms must operate consistently despite extreme cold.
At Alba Manufacturing, designing heavy-duty conveyor equipment for these demanding conditions is nothing new. Decades of engineering experience and more than 15 years of successful electro-hydraulic applications have helped Alba develop freezer-rated conveyor systems that deliver dependable performance.
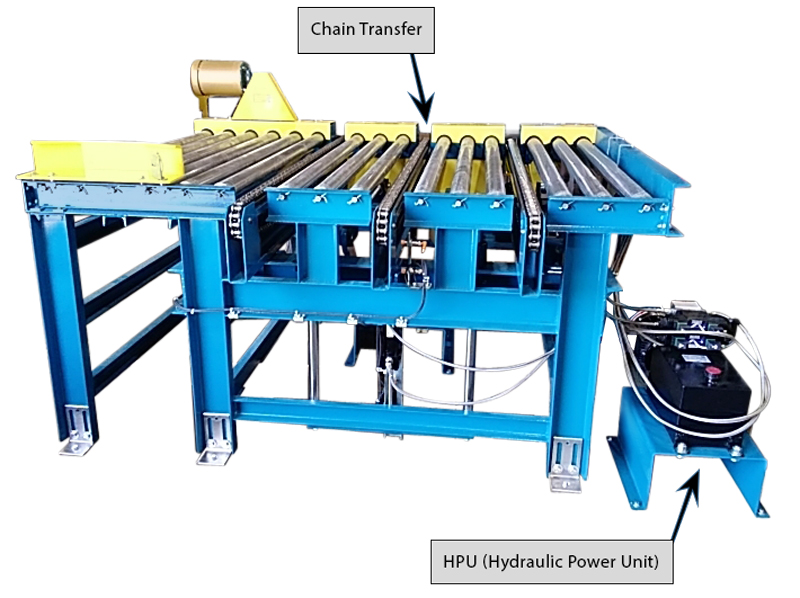
One important engineering decision involves how Alba raises and lowers its 90° pop-up chain transfers.
While some manufacturers rely on electro-mechanical actuators, Alba has found that electro-hydraulic lifting systems provide a more reliable, efficient, and practical solution for heavy-duty freezer applications.

Why Alba Moved Away from Electric Actuators |
|
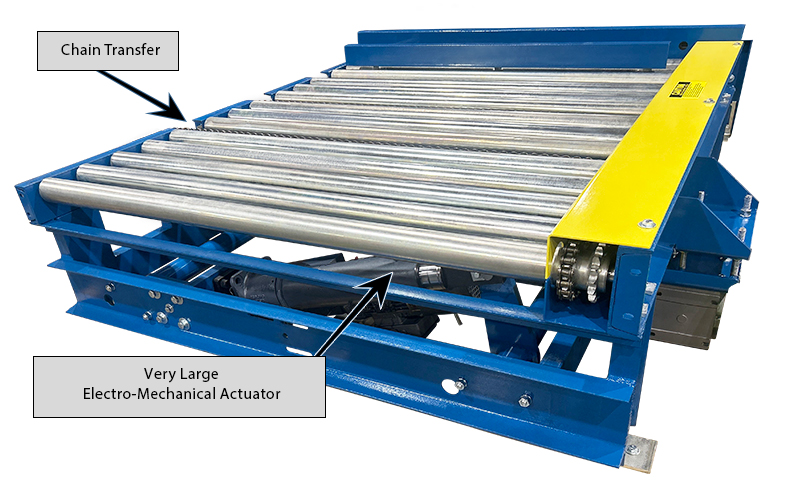
Earlier Alba transfer designs incorporated motorized ball screw and acme screw assemblies driven by electric motors. Although these systems could perform the required lifting functions, experience revealed several disadvantages, particularly in subzero environments.
Electro-mechanical lifting systems could require 15 seconds or more to complete a lift-and-lower cycle. They also required precise controls to prevent overtravel, mechanical damage, and potential shear pin failures.
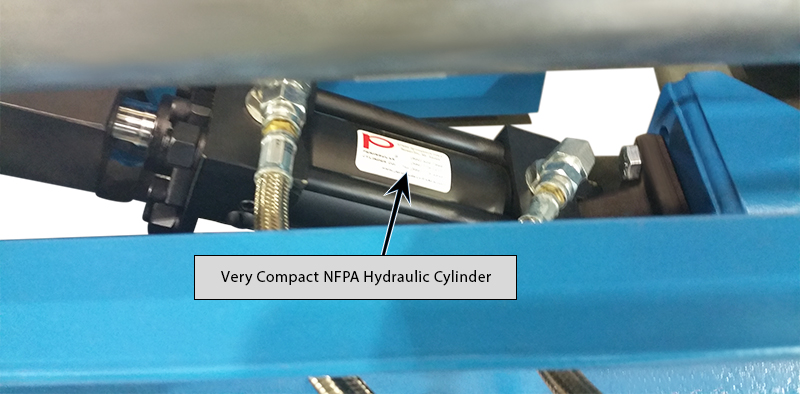
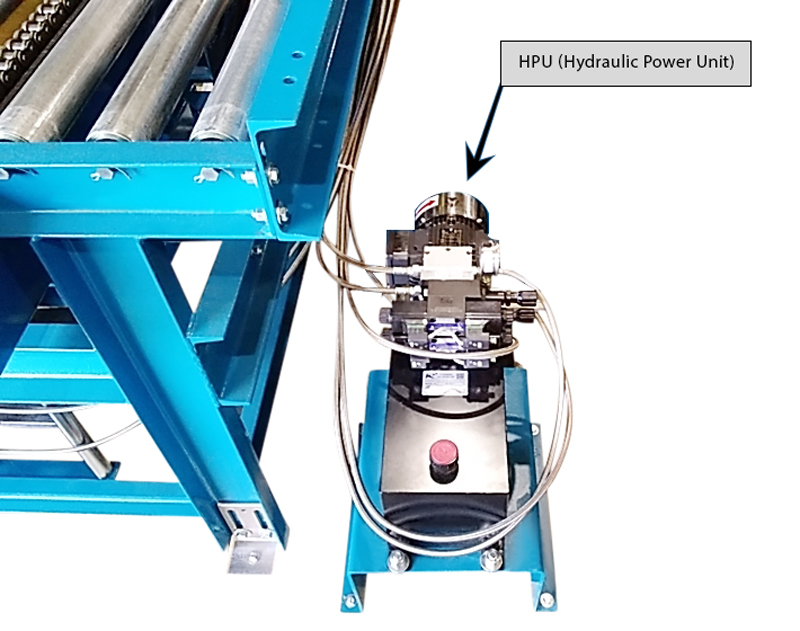
As these challenges became apparent, Alba refined its approach by incorporating hydraulic cylinders powered by remotely mounted Hydraulic Power Units (HPUs).
The result was a lifting system better suited to the demands of continuous heavy-duty pallet handling.
The Advantages of Electro-Hydraulic Transfers |
|
Alba's hydraulic lifting systems offer several important advantages over the electro-mechanical configurations previously used in its freezer applications.
Faster, More Consistent Operation |
|
Hydraulic cylinders provide smooth, controlled lifting and lowering without the extended cycle times associated with Alba's earlier electric screw-driven systems. Faster transfer cycles can contribute to improved overall conveyor throughput.
Four-Point Positive Lifting |
|
Alba's proven four-point positive lifting mechanism maintains balanced, synchronized movement across the transfer. This is especially important when handling heavily loaded pallets that must be raised evenly before changing direction by 90°.
Compact, Heavy-Duty Construction |
|
Hydraulic cylinders are generally more compact than comparable electric actuator assemblies, allowing Alba to maintain a lower-profile transfer design without sacrificing the lifting capability required for demanding applications.
Reduced Mechanical Complexity |
|
Electro-mechanical systems depend on screw mechanisms, motors, limit controls, and other components that can become maintenance concerns in freezer environments. Alba's hydraulic configuration reduces reliance on these mechanisms while providing dependable lifting performance.
Remote Hydraulic Power Units |
|
One of the most practical advantages is the ability to locate HPUs away from the transfer mechanism. Depending on system configuration, this can improve maintenance accessibility and simplify service.
Standardized Components |
|
Alba incorporates NFPA-interchangeable hydraulic cylinders, providing familiar, standardized components that can simplify replacement and reduce maintenance complications.
Freezer-Compatible Hydraulic Fluids |
|
The hydraulic circuits use fluids selected for low-temperature performance, with food-grade options available when required. Flexible hydraulic hoses connect the cylinders to their power units.
Flexible System Configuration |
|
A single HPU can be configured to operate multiple devices, including pop-up chain transfers and blade stops. This gives system designers additional flexibility when developing automated pallet handling solutions.
Designing the Entire Conveyor System for Freezer Conditions |
|
Although hydraulic lifting systems are an important part of Alba's freezer-rated equipment, reliable operation requires much more than selecting the right transfer mechanism.
Every component must be evaluated for how it will perform in freezing temperatures.
Alba addresses these challenges with freezer-rated equipment and components that include:
| • |
Zinc-Plated Rollers and Axles |
| Provide durability and corrosion resistance in demanding operating environments. |
| • |
Nylatron Wear Strips
|
| Support smooth chain movement while reducing friction along conveyor chain rails. |
| • |
Freezer-Rated Motors and Gearmotors |
| Deliver dependable power and torque in subzero applications. |
| • |
Freezer-Rated Bearings |
| Address low-temperature lubrication requirements and operating conditions. |
| • |
Freezer-Rated Sensors |
| Include photo-eyes and proximity sensors selected for reliable operation in cold environments. |
| • |
Freezer-Rated Scissor Lifts |
| Provide controlled lifting and positioning within automated pallet handling systems. |
| • |
Freezer-Rated Turntables |
| Accommodate directional changes and load positioning in freezer conveyor applications. |
| • |
Adjustable Jack-Bolt Feet |
| Provide stable equipment support and allow adjustment for uneven floors. |
By considering the entire conveyor system rather than individual components alone, Alba helps integrators develop material handling solutions engineered for long-term performance.
Experience Matters When Temperatures Drop |
|
Selecting conveyor equipment for a freezer application involves more than confirming that individual components carry a low-temperature rating.
The equipment must function as a complete system, repeatedly handling heavy pallet loads while maintaining reliable operation, cycle efficiency, and serviceability.
Alba's transition from electro-mechanical to electro-hydraulic lifting systems illustrates the value of real-world engineering experience. Rather than relying solely on theoretical performance, Alba has refined its designs based on what works in demanding operating environments.
The result is heavy-duty freezer-rated conveyor equipment engineered for dependable performance when temperatures reach -20°F.
For system integrators and end users evaluating freezer conveyor applications, Alba Manufacturing offers the engineering expertise, equipment, and practical experience to help develop the right solution.
Contact your Regional Sales Manager or locate an Alba Partner Network member in your area. You can also call 866.252.2634 or visit www.albamfg.com to discuss your freezer-rated pallet handling requirements. |