When it comes to heavy-duty pallet handling, not all chain transfers are created equal. While many manufacturers offer equipment capable of moving pallets 90 degrees, the real difference is how reliably that equipment performs under heavy loads, repeated cycling, and demanding industrial conditions.
Alba Manufacturing has established a reputation for building rugged, dependable pallet handling equipment. Its heavy-duty chain transfers reflect that philosophy, combining robust construction, a mechanically controlled positive-lift system, and application-specific engineering.
So, are Alba Chain Transfers the best in the industry? Consider what goes into their design.
A Positive-Lift System That Makes the Difference
One of the most important features distinguishing Alba Chain Transfers is their four-point positive-lift mechanism.
Unlike transfer designs that rely on inflatable air bags to raise and lower loads, Alba uses a heavy-duty mechanical lifting arrangement driven by a pneumatic cylinder.
The cylinder activates pivot arms connected by a tie-rod, creating a controlled lifting motion that raises and lowers the transfer carriage evenly.
This design helps keep pallet loads level and properly supported throughout the transfer cycle.
That matters when handling pallets weighing thousands of pounds. Uneven lifting can cause loads to shift, pallets to become misaligned, and equipment to jam. Alba’s positive-lift design helps minimize these risks while supporting consistent, repeatable operation.
Heavy-Duty Construction Without Compromise
A chain transfer is only as dependable as the structure supporting it.
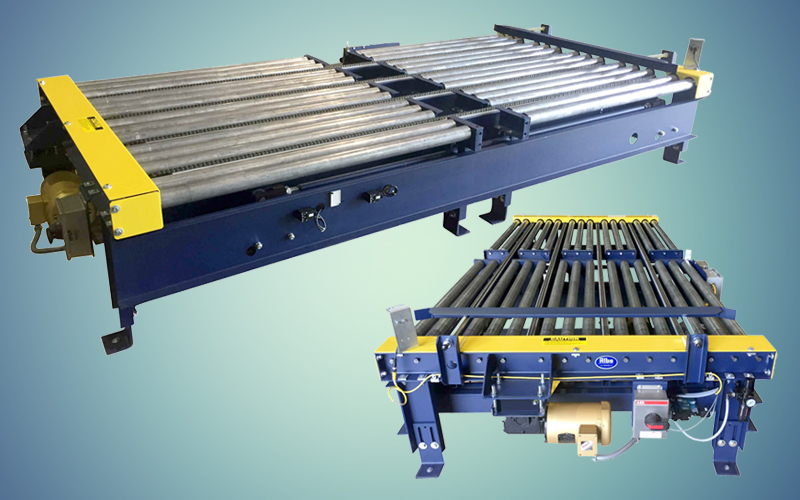
Alba builds its standard chain transfers with welded structural steel frames rather than relying on lightweight construction. Heavy-duty transfer carriages, continuously welded sprockets, and adjustable channel supports provide the strength and rigidity needed for demanding industrial applications.
Standard Alba Chain Transfers accommodate loads up to 4,000 pounds.
These features are designed to withstand repeated operating cycles while helping reduce mechanical wear, maintenance requirements, and unexpected downtime.
For manufacturers and distribution centers, that translates into equipment built for long-term performance rather than simply meeting minimum specifications.
Four Configurations for Different Applications
Every pallet handling system has unique requirements. Conveyor layouts, pallet construction, directional changes, and equipment integration all influence the appropriate transfer design.
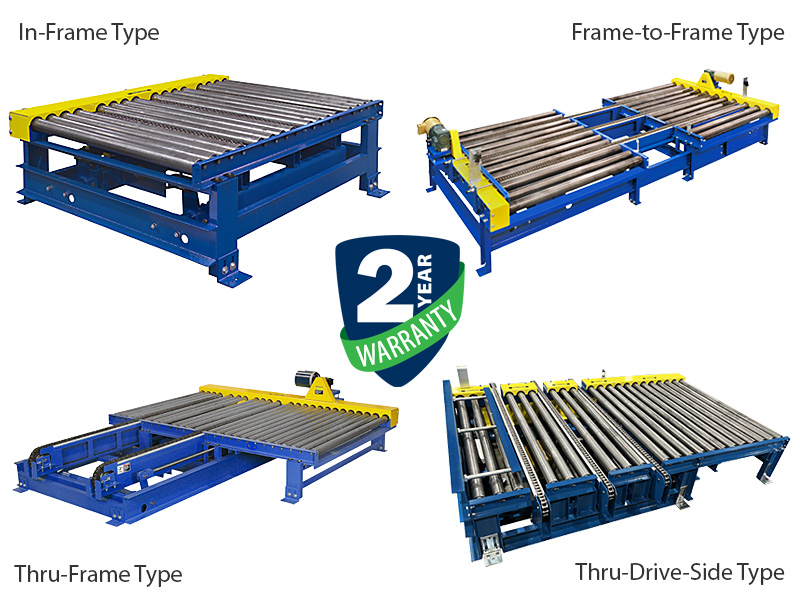
Alba addresses these differences with four standard configurations:
- In-Frame: Transfer mechanism contained within the conveyor frames.
- Thru-Frame: Transfer chains extend beyond the non-driven side of the conveyor.
- Frame-to-Frame: Designed to transfer loads between parallel conveyor sections.
- Thru-Drive-Side: Transfer chains extend through the conveyor drive side, providing additional layout flexibility.
These configurations allow engineers and system integrators to select equipment that fits their specific applications without sacrificing heavy-duty construction.
Engineered for Dependable Operation
Reliable pallet handling requires more than structural strength.
Alba Chain Transfers incorporate properly sized drives, heavy-duty transfer chains, and controls designed to support consistent operation.
Standard equipment includes solenoid valves and proximity switches for monitoring raised and lowered transfer positions.
Additional options, including pallet stops, backstops, transition rollers, forklift barriers, and specialized finishes, allow each transfer to be configured for its operating environment.
Alba also offers hydraulic lifting options for applications where pneumatic operation may not be practical, including certain freezer environments.
Factory Testing and Installation Advantages
Even well-engineered equipment needs to operate correctly when installed.
Alba’s standard chain transfers are shipped fully assembled and factory-tested before delivery, helping simplify installation and reduce potential startup problems.
A standard two-year warranty provides additional confidence in the equipment and the manufacturer’s commitment to quality.
So, Are Alba Chain Transfers the Best?
There is no single chain transfer that is best for every application. However, Alba makes a compelling case for being among the industry’s best heavy-duty pallet transfer manufacturers.
Its combination of four-point positive lifting, welded structural steel construction, multiple configurations, application-specific engineering, and factory testing addresses the factors that matter most: load stability, durability, reliability, and long-term operating performance.
When a chain transfer handles thousands of pounds, repeatedly and reliably, the quality of its engineering becomes more than a selling point. It becomes an essential part of keeping production moving.
For heavy-duty pallet handling applications where dependable performance is nonnegotiable, Alba Chain Transfers deserve serious consideration.
Learn more about Alba Manufacturing’s Chain Transfers or call 866-252-2634 to discuss your application.