How Alba and CS Robotics Engineered a Reliable Palletless Handling System for an Automated Palletizing Operation
The Challenge: Increasing Production Without Increasing Manual Handling
A sunflower seed producer was experiencing significant production growth but faced a growing challenge: finding enough employees to manually stack packaged products and transfer completed pallet loads. To maintain production efficiency and reduce dependence on manual labor, the company turned to automation.
Integration partner CS Robotics was tasked with developing a robotic palletizing system capable of handling the increased production volume. However, the application presented an unusual material handling challenge.
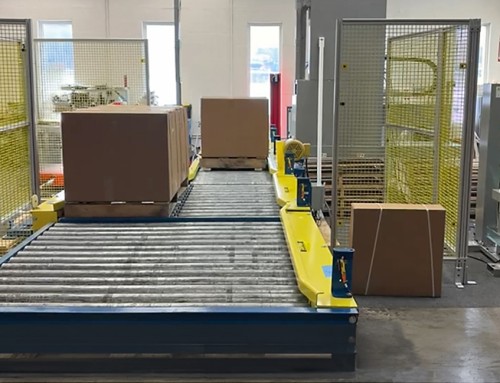
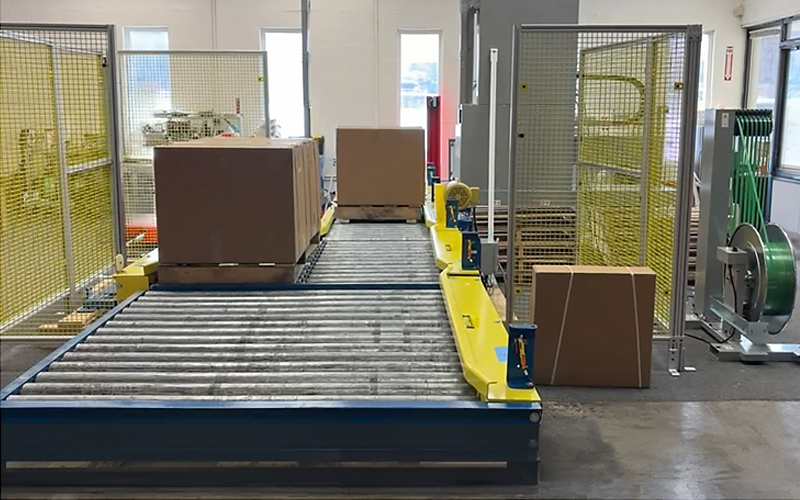
Unlike conventional palletizing systems, the producer’s operation would not use wooden pallets to support completed loads. Instead, the robotic palletizer would place packaged sunflower seed products directly onto 42″ x 50″ corrugated slip sheets resting on conveyor rollers.
With loads weighing up to 2,000 pounds and no rigid pallet underneath, maintaining load stability throughout the conveying process was critical. The system needed to transport these unsupported loads through multiple conveyor sections and directional changes without disturbing the product.
The Solution: Heavy-Duty Conveyors Designed for Smooth Product Transfers
CS Robotics partnered with Alba Manufacturing to develop a conveyor system specifically engineered for the application’s unique requirements.
Before finalizing the equipment design, the end user shipped representative products and corrugated slip sheets to Alba for proof-of-concept testing. The objective was to confirm that the unsupported loads could travel across the conveyor rollers while maintaining their stability and integrity.
Following successful testing, Alba supplied a complete conveyor solution consisting of:
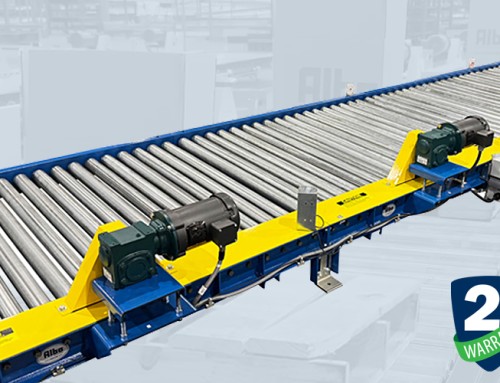
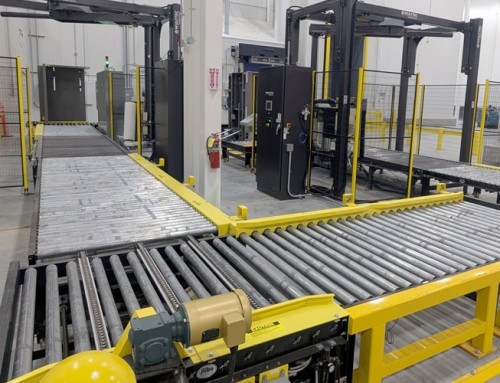
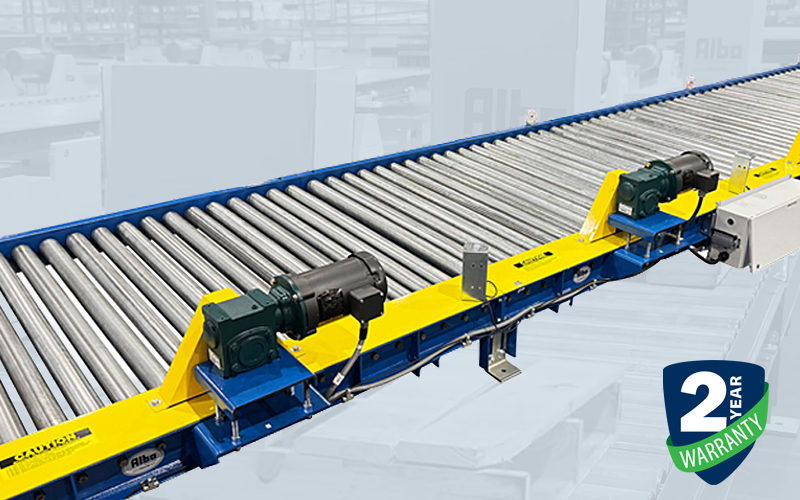
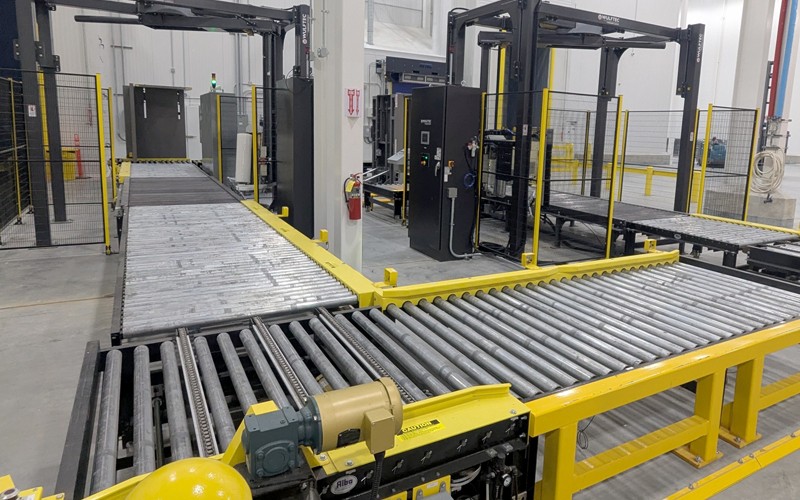
- Eight sections of Chain Driven Live Roller Conveyor (CDLR) to transport the palletless loads.
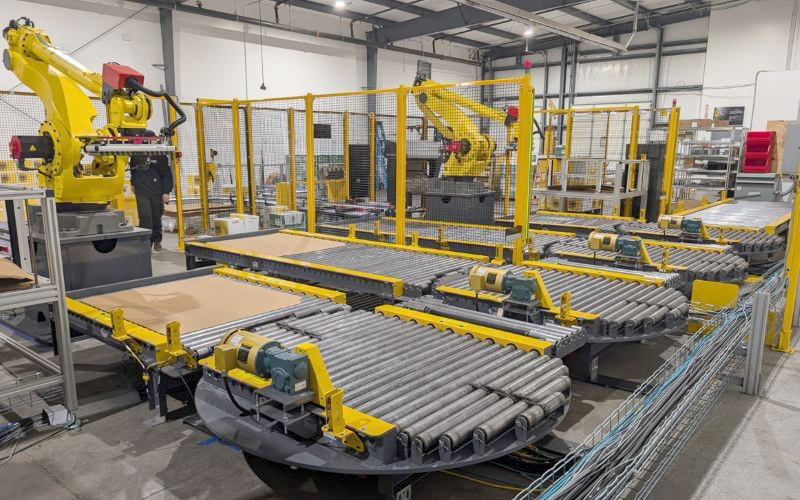
- Two CDLR Turntables to provide smooth directional changes without the disruption associated with conventional pop-up transfers.
- Close roller spacing to maintain consistent support beneath the corrugated slip sheets.
- Conveyor-mounted and floor-mounted transition rollers to minimize gaps between equipment sections and maintain smooth product movement.
The decision to use turntables instead of conventional pop-up transfers was particularly important. Because the loads rested directly on corrugated slip sheets, abrupt lifting or transferring movements could compromise stability. The turntables allowed loads to change direction while remaining consistently supported.
Every component was selected and configured to minimize product disturbance and support dependable operation throughout the automated palletizing process.

The Results: Verified Performance and Simplified System Integration
Alba’s proof-of-concept testing confirmed that the slip sheets and unsupported loads could be conveyed successfully, giving CS Robotics and the end user greater confidence before committing to the final system design.
The resulting conveyor solution provided the sunflower seed producer with a practical way to accommodate increased production while reducing the manual handling associated with stacking products and transferring pallets.
Beyond the equipment’s performance, CS Robotics valued Alba’s heavy-duty construction and installation-ready design. Rather than receiving individual components requiring extensive field assembly, the integrator received completed conveyor sections ready for integration into the automated system.
As CS Robotics explained:
“Alba sends us a completed conveyor—not an erector set.”
This approach helped simplify installation and reduce the amount of assembly required at the customer’s facility.
The project demonstrated how careful engineering, application-specific equipment design, and upfront product testing can address challenging material handling requirements while reducing uncertainty during system development.
The Alba Advantage: Engineering Confidence Into Every Application
Palletless unit-load handling requires more than conventional conveyor equipment. It demands an understanding of load characteristics, product stability, roller support, and transfer methods.
By combining proof-of-concept testing with rugged CDLR conveyors, heavy-duty turntables, and carefully engineered transitions, Alba Manufacturing helped CS Robotics deliver a solution designed around the specific demands of the sunflower seed producer’s operation.
The project also highlights the value of working with an experienced conveyor manufacturer that provides fully assembled, integration-ready equipment rather than leaving extensive construction and troubleshooting to the installation team.
Have a challenging pallet handling application?
Alba Manufacturing works with integrators and equipment manufacturers to develop durable, application-specific conveyor solutions for demanding production and distribution environments.
Conveyor/Product Specifications
- Product: Packaged Sunflower Seed Unit Loads Conveyed on 42″ Wide x 50″ Long Corrugated Slip Sheets, 2,000 lb. Maximum Weight
- Chain Driven Live Roller Conveyor: Model No. 251140-2.75-DBS, Driven Both Sides
- Conveyor Sections:
- Six (6) Sections, 4’11” Long
- Two (2) Sections, 9’11-1/2″ Long
- Effective Width: 48″ Effective Conveying Surface
- Motor: 1/2 HP Baldor Super “E” Motor
- Speed: 30 FPM @ 60 Hz
- Elevation: 18″ Top of Roller
- Paint: RAL 7015 Slate Grey with RAL 1003 Signal Yellow Chain Guards
- Turntables: Model No. TT251140-2.75-DBS CDLR Turntable Tops with Electric Rotation Bases:
- Four (4) 75″ Diameter Turntables
- 48″ Effective Conveying Surface
- 1/2 HP Baldor Super “E” Motor for the CDLR Conveyor
- 1 HP Gearmotor with Brake for Turntable Rotation
- 18″ Top of Roller
- 30 FPM @ 60 Hz
- RAL 7015 Slate Grey with RAL 1003 Signal Yellow Chain Guards
Value Added Features
- Five (5) Special Sets of Conveyor-Mounted Transition Rollers with Eight (8) Rollers per Set
- Three (3) Sets of Floor-Mounted Transition Roller Stands to Fill the Gaps Between Turntables
- Fixed End Stops
- Motor Disconnects Mounted to the Conveyors and Wired to the Motors
- Special Paint Colors
About Us
Alba Manufacturing, established in 1973, engineers and designs heavy-duty roller conveyor systems. Our systems consist of chain driven live roller (CDLR), zero pressure accumulation, drag chain, gravity, lift and rotate, pallet stackers and dispensers, turntables, chain transfers and transfer cars. Our corporate office and manufacturing facility is located in Fairfield, Ohio, approximately 30 minutes north of Cincinnati, Ohio.
For more information regarding this application/solution, please contact us via phone at 866.252.2634; via web at www.albamfg.com or via email at RockSolidConveyor@albamfg.com.