Alba Manufacturing Integrates Heavy-Duty CDLR Conveyors with Automated Door Controls for Safe, Efficient Material Movement
The Challenge
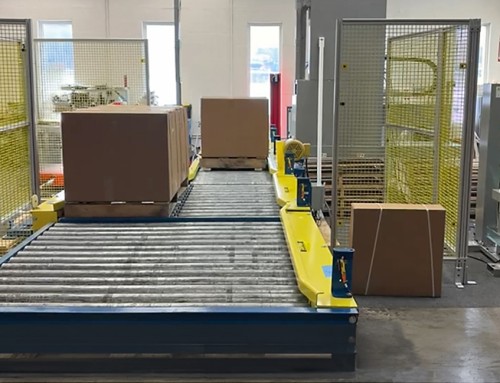
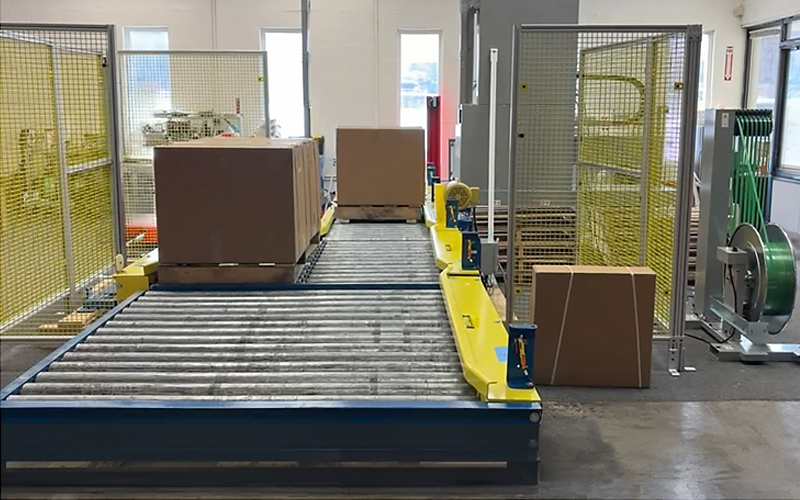
A customer needed a reliable way to move valuable palletized products from a secure storage cage into the main warehouse for forklift pickup. The application required a conveyor system that could coordinate with an automated roll-up door while maintaining security, improving material flow, and protecting operators during loading and unloading.
Working with a long-time integrator partner, Alba Manufacturing was tasked with developing a heavy-duty pallet handling solution that would simplify installation, minimize onsite wiring, and provide dependable operation.
The Solution
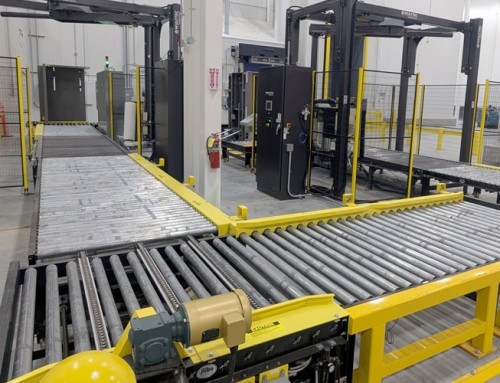
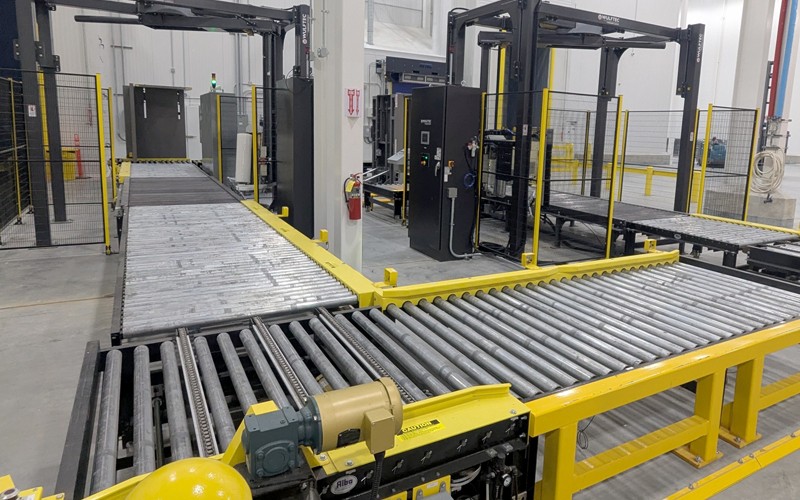
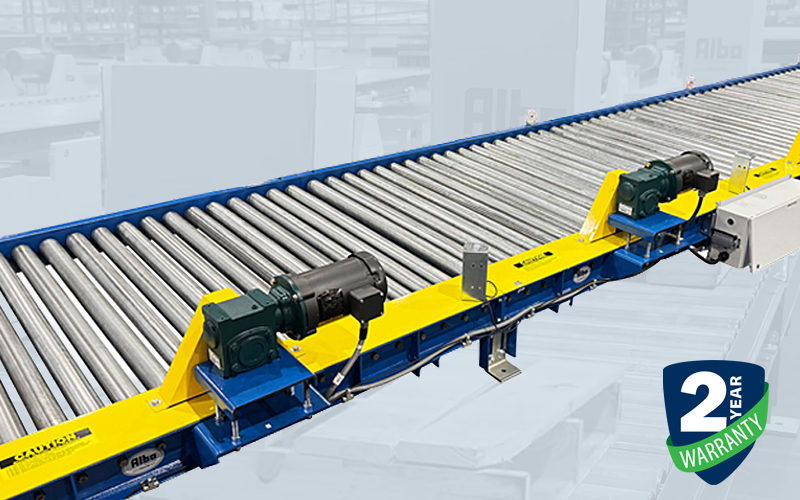
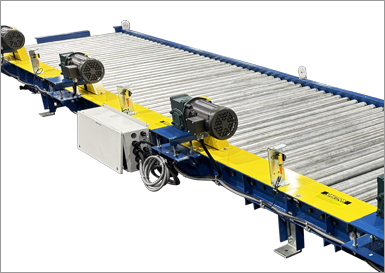
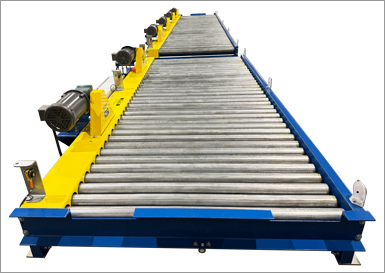
Alba designed a six-zone Chain Driven Live Roller (CDLR) conveyor system equipped with its standard plug-and-play Motorized Zero Pressure Accumulation (MZPA) controls.
Each conveyor zone was powered by a 1/2 HP Baldor C-frame motor and Dodge Tigear II gear reducer, operating at 30 feet per minute. Heavy-duty adjustable supports allowed precise conveyor elevation to accommodate the installation requirements.
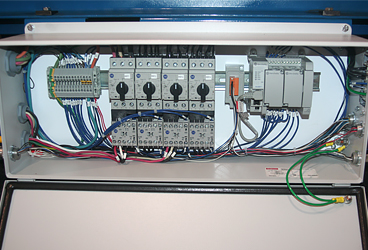
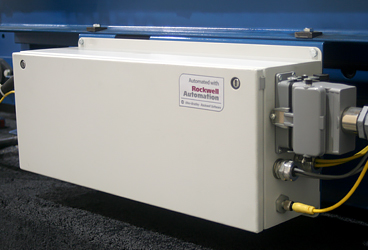
To simplify system integration, Alba incorporated an Allen-Bradley Micro PLC with pre-installed programming. Quick-disconnect cables streamlined the electrical connections, while a single power drop supplied the main control enclosure. This plug-and-play approach significantly reduced the need for extensive field wiring and programming.
Integrating Security and Safety
A critical element of the application was coordinating pallet movement with the automated roll-up door separating the secure cage from the warehouse.
Alba programmed the system to stop pallets in Zone 2 and send a “pallet present” signal to the door controller. Once the door opened, the conveyor received a “Run” signal, allowing the pallet to advance into Zone 3.
This sequence provided controlled pallet movement between the two areas without compromising the intended security process.
Operator safety was another important consideration. Ultrasonic sensors positioned at the conveyor infeed and discharge detected forklift presence and stopped conveyor movement during loading and unloading. This prevented pallets from moving while being handled by a forklift, reducing the potential for equipment damage and operator hazards.
The Results
The completed system provided an efficient, easy-to-operate solution for transferring palletized products from secure storage into the warehouse.
Alba’s six-zone accumulation design helped regulate pallet flow while reducing unnecessary forklift movement. Integration with the automated door provided controlled product transfer, and the ultrasonic sensors added an important layer of operator protection.
The plug-and-play MZPA controls also simplified installation, reduced onsite electrical integration requirements, and delivered a practical, cost-effective approach to automated pallet handling.
Key benefits included:
- Improved Workflow: Six independently controlled accumulation zones supported efficient pallet movement and staging.
- Enhanced Safety: Ultrasonic sensors stopped conveyor movement during forklift interaction.
- Automated Door Integration: Coordinated controls ensured pallets advanced only after the roll-up door opened.
- Simplified Installation: Pre-programmed controls and quick-disconnect wiring minimized onsite integration work.
- Heavy-Duty Reliability: Rugged CDLR construction and proven components supported demanding pallet handling operations.
Engineered for Real-World Applications
This project demonstrates Alba Manufacturing’s ability to combine heavy-duty conveyor equipment with practical automation solutions that address specific operational requirements.
By integrating reliable mechanical components, intelligent accumulation controls, and operator safety features, Alba and its integrator partner delivered a system designed to improve material flow while simplifying installation and operation.
Conveyor/Product Specifications
- Product: 40″ x 48″ Wood GMA Pallets, 2,000 lb. Maximum Weight
- Length: 29’10” Long Line Consisting of Six (6) Zones @ 4′ 11-1/4″ Overall with a 2-1/2″ Wide Door Gap
- Rollers:
- 2-1/2″ Diameter x 11 Gauge Wall, 11/16″ Hex Axles, Spring Retained, #40A21 Sprockets, Grease Packed Ball Bearings
- On 3-1/4″ Roller Centers
- Effective Width: 52″ Effective Conveying Surface
- Motor:
- 1/2 HP, Baldor C-Frame Motor and Dodge Tigear II Gear Reducer, 230/460/3/60, RC-40 Drive Chain, Under Slung Mounted Drive
- Speed: 30 FPM, Fixed
- Elevation: 11″ Top of Roller
- Paint: Alba Blue with Safety Yellow Chain Guards
- Standard Items included:
- End Stop: Fixed Channel End Stops with Fork Cutouts
Value-Added Features
- Two (2) Conveyors include a Floor Mounted Fork Truck Wheel Stop x 5’0″ Long Painted Safety Yellow
- Alba’s Standard MZPA Zero Pressure Accumulation Control Package
- Ultra Sonic Sensors Mounted to Conveyor Frame at the Fork Truck Load and Unload Zones
- E-Stop: System includes an E-stop Safety Circuit including Allen Bradley Safety Relay
About Us
Alba Manufacturing, established in 1973, engineers and designs heavy-duty roller conveyor systems. Our systems consist of chain driven live roller (CDLR), zero pressure accumulation, drag chain, gravity, lift and rotate, pallet stackers and dispensers, turntables, chain transfers and transfer cars. Our corporate office and manufacturing facility is located in Fairfield, Ohio, approximately 30 minutes north of Cincinnati, Ohio.
For more information regarding this application/solution, please contact us via phone at 866.252.2634; via web at www.albamfg.com or via email at RockSolidConveyor@albamfg.com.