How Alba Manufacturing and Innovative Conveyor Concepts Delivered a More Reliable Pallet Handling Solution
The Challenge
An industrial packaging operation needed to modernize an aging pallet conveyor system that was causing frequent downtime, increasing maintenance requirements, and limiting production efficiency.
The facility operated three conventional palletizers, each handling multiple case configurations and feeding completed pallet loads into a stretch-wrapping process. The original material handling system utilized a drag chain conveyor with pop-up roller transfers running down the center of the palletizing line.
Although the equipment had operated for many years, mechanical wear and aging components were becoming increasingly problematic. The system also struggled to accommodate the different pallet types moving through the operation.
The customer needed a more reliable, flexible conveyor solution that would improve pallet movement, reduce maintenance demands, and integrate with the existing palletizers and stretch wrapper.
The Solution
Innovative Conveyor Concepts, Inc. (ICC), a member of the Alba Partner Network (APN), partnered with Alba Manufacturing to design and implement a modernized pallet handling system utilizing Alba’s heavy-duty roller conveyor equipment and ICC’s integrated control technology.
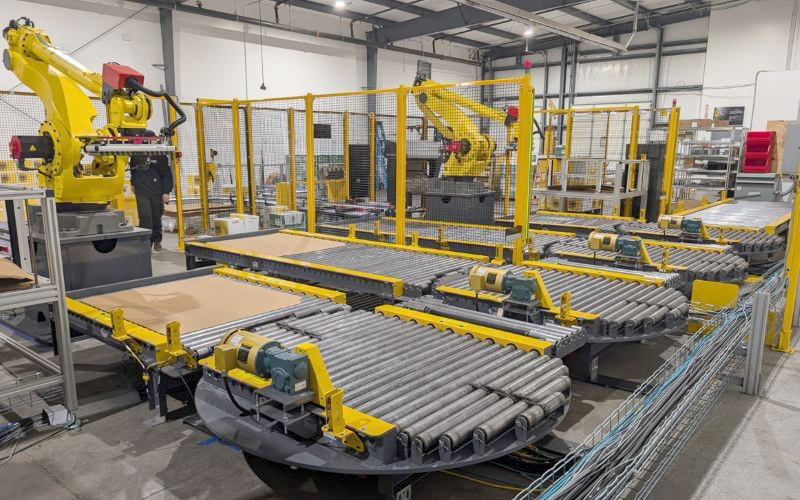
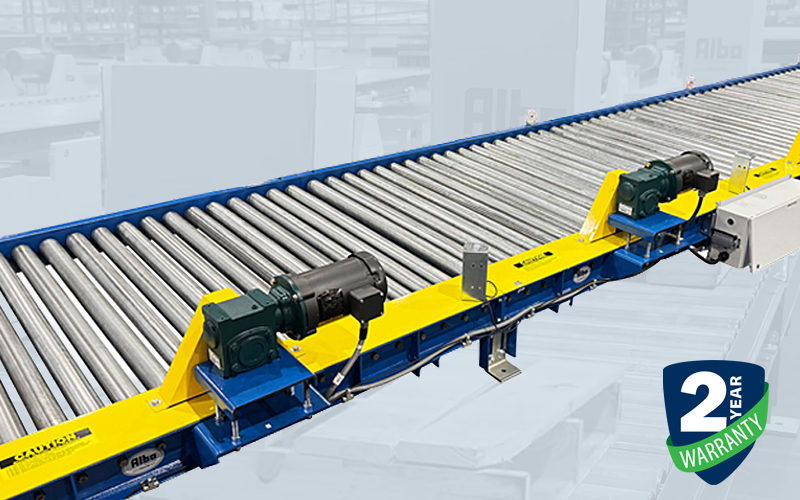
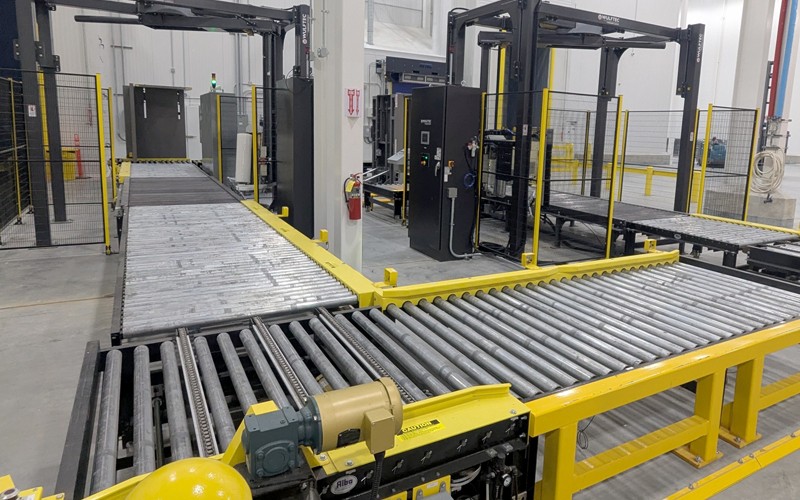
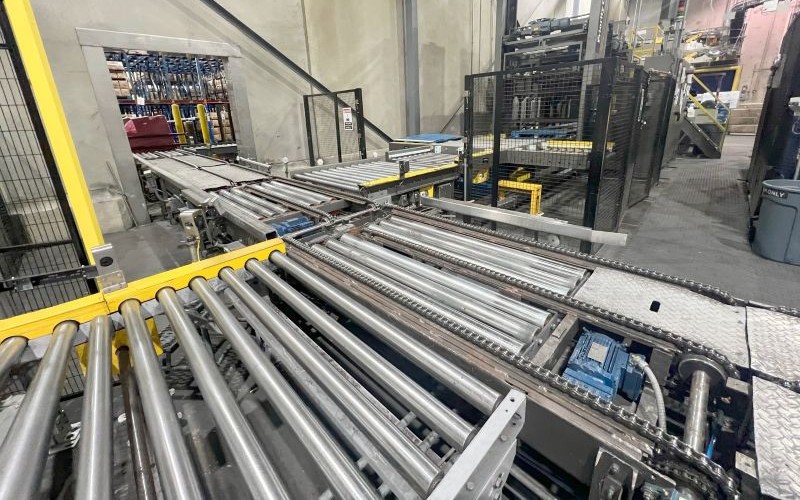
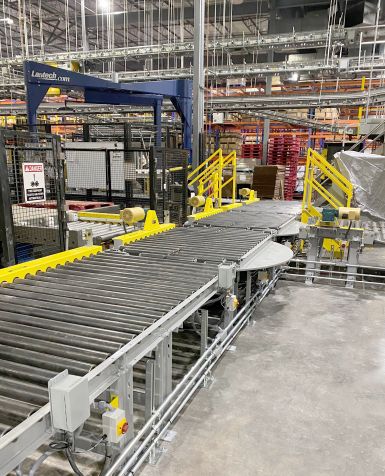
The redesigned system replaced the aging drag chain configuration with a roller-based conveyor arrangement engineered to provide smoother pallet movement and accommodate varying pallet configurations.
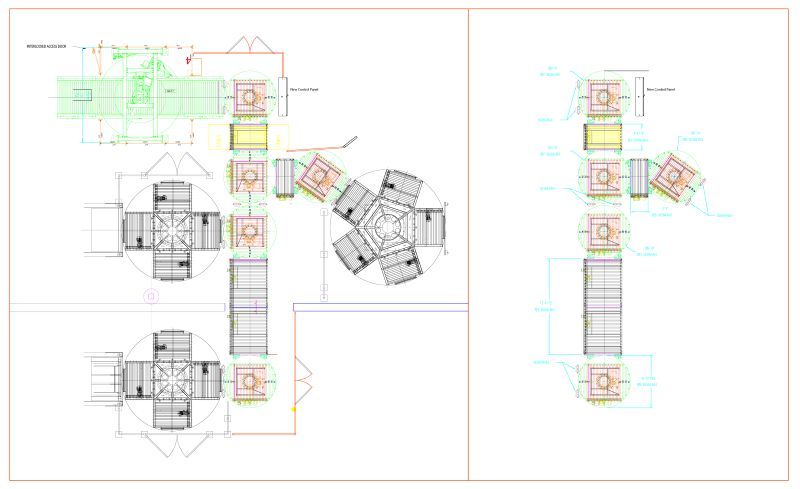
Beginning at the first of three palletizers, the new conveyor system transports pallets through the packaging operation using an automated, controlled-flow approach. ICC developed an integrated control system that coordinates pallet traffic and communication between the palletizers and downstream equipment.
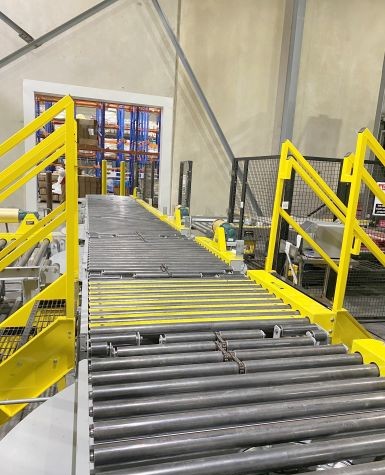
One important design consideration involved maintaining safe operator access across the production line. Alba engineered a specialized operator crossover conveyor section positioned between the fourth and fifth turntables. This arrangement allows personnel to cross the production area while maintaining efficient pallet movement.
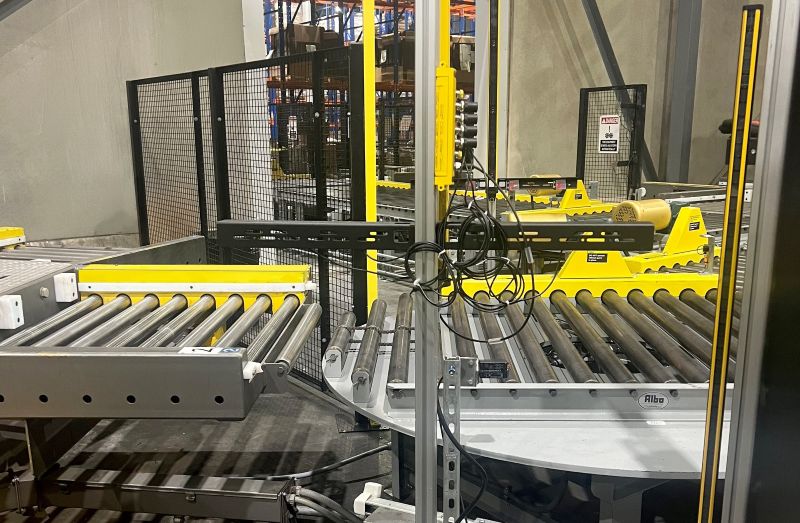
At the discharge end of the system, an Alba 90° turntable redirects pallets into the facility’s existing stretch wrapper. ICC incorporated a controls handshake between the conveyor system and stretch wrapper to coordinate equipment operation and maintain consistent product flow through the final packaging stage.
The combination of Alba’s heavy-duty conveyor engineering and ICC’s system integration expertise provided a practical solution to the facility’s existing operational challenges.
The Results
The completed conveyor modernization delivered several important operational improvements:
- Improved Reliability: Replacing aging equipment with heavy-duty roller conveyors reduced the mechanical issues associated with the original system.
- Reduced Maintenance Requirements: The updated conveyor design simplified pallet handling and reduced maintenance demands.
- Greater Pallet Handling Flexibility: The roller-based configuration better accommodates the different pallet types processed through the facility.
- Improved Production Flow: Integrated controls coordinate pallet movement between the three palletizers and the stretch-wrapping operation.
- Safer Operator Access: Alba’s engineered crossover section provides a designated route across the production line.
- Long-Term Durability: Heavy-duty construction provides a dependable foundation for continued operation.
For the customer, the modernization resulted in a more reliable and manageable pallet handling operation, helping reduce unplanned downtime while supporting consistent production.
The Alba Advantage
This project demonstrates the value of combining Alba Manufacturing’s heavy-duty conveyor engineering with the application knowledge and controls expertise of its Alba Partner Network integrators.
By working together, Alba and ICC transformed an aging, maintenance-intensive conveyor system into a modern pallet handling solution designed for improved reliability, flexibility, and long-term performance.
When aging conveyor equipment begins affecting production, Alba Manufacturing and its APN partners can help develop a practical solution.
Conveyor/Product Specifications
- CDLR Conveyor: Model 29760-4.5 CDLR Conveyor. Lengths: One (1) – 2′ 3″ Long, One (1) – 3′ 4-1/2″ Long, One (1) – 6′ 0″ Long & One (1) – 6′ 4-1/2″ Long
- Turntables: Turntables with Electric Rotation Bases, 30-1/2″ Top of Roller, 45 FPM @ 60 Hz, 90° Rotation on Four (4) Turntables, 36° Rotation on One (1) Turntable
- Rollers: 2-9/16″ x 7-Gauge Rollers with Heavy-Duty Bearings
- Effective Width: 52″
- Motor: 1 HP Baldor Super-E Motors
- Paint: RAL 7042 (Transfer Grey) Color Match
- Standard Items Included: Gravity Transition Rollers Mounted to the Conveyor
Value Added Features
- Conveyor Crossover
- Banner 24 VOC Diffused Photo Eyes Wired to a Junction Box
About Us
Alba Manufacturing, established in 1973, engineers and designs heavy-duty roller conveyor systems. Our systems consist of chain driven live roller (CDLR), zero pressure accumulation, drag chain, gravity, lift and rotate, pallet stackers and dispensers, turntables, chain transfers and transfer cars. Our corporate office and manufacturing facility is located in Fairfield, Ohio, approximately 30 minutes north of Cincinnati, Ohio.
For more information regarding this application/solution, please contact us via phone at 866.252.2634; via web at www.albamfg.com or via email at RockSolidConveyor@albamfg.com.