How Alba Manufacturing and Advanced Equipment Company Engineered a Heavy-Duty Pallet Handling Solution for -20°F Conditions
The Challenge
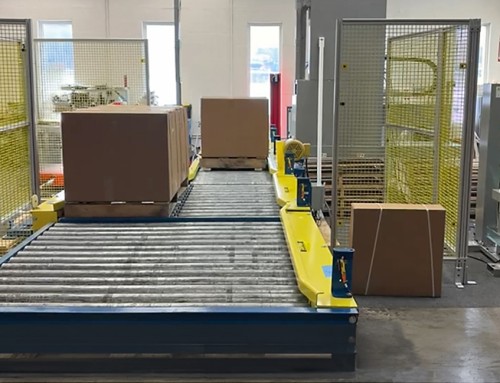
A cold storage operation required an automated pallet handling system capable of moving heavy palletized loads into and out of a -20°F freezer environment. The system needed to accommodate both 40″ x 48″ CHEP and GMA pallets carrying loads weighing up to 2,500 pounds.
Advanced Equipment Company (AEC), an Alba Manufacturing integration partner with extensive experience in cold storage automation, needed a conveyor solution that could withstand extreme temperatures while integrating seamlessly into the customer’s automated material handling system.
Beyond the temperature requirements, the application presented additional challenges involving forklift interaction, pallet positioning, equipment protection, and long-term durability. The conveyor equipment also needed to integrate with AEC’s pallet down-ender design without compromising system performance or operational efficiency.
The Solution
AEC partnered with Alba Manufacturing to develop a rugged, freezer-ready conveyor system engineered specifically for the application.
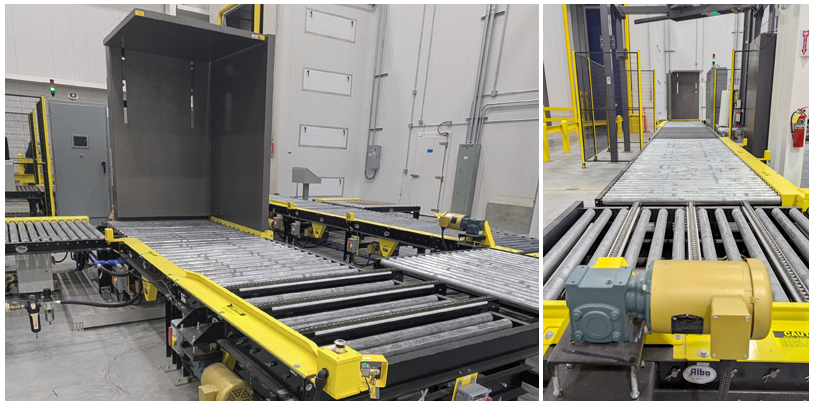
Alba supplied a comprehensive package of heavy-duty pallet handling equipment, including:
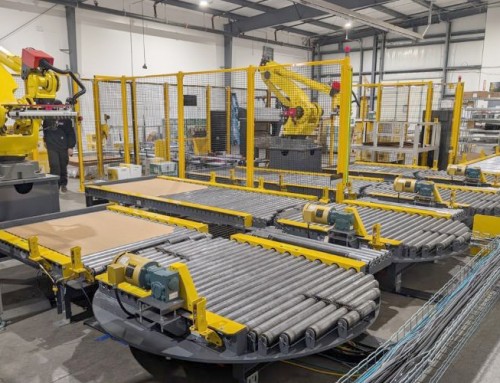
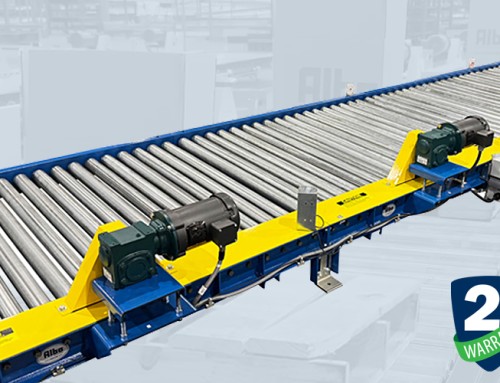
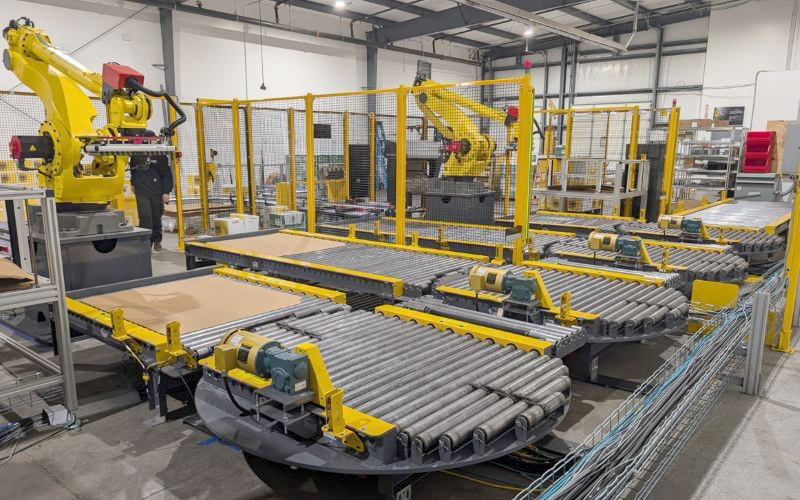
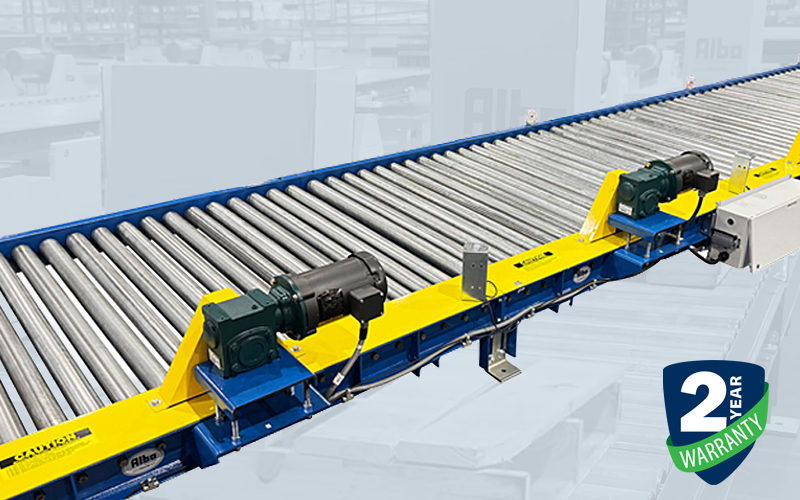
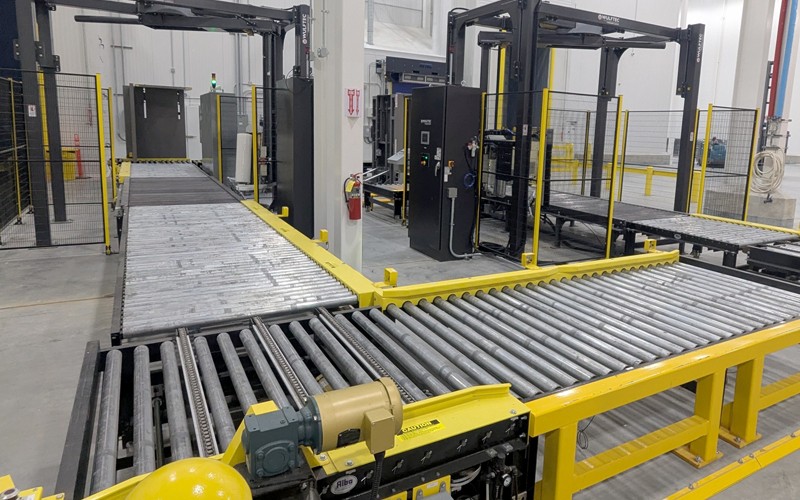
- Chain Driven Live Roller (CDLR) Conveyors
- Thru-Frame and Thru-Drive-Side Transfers
- Hydraulic-Actuated Chain Transfers
- Low-Temperature-Rated Conveyor Sections
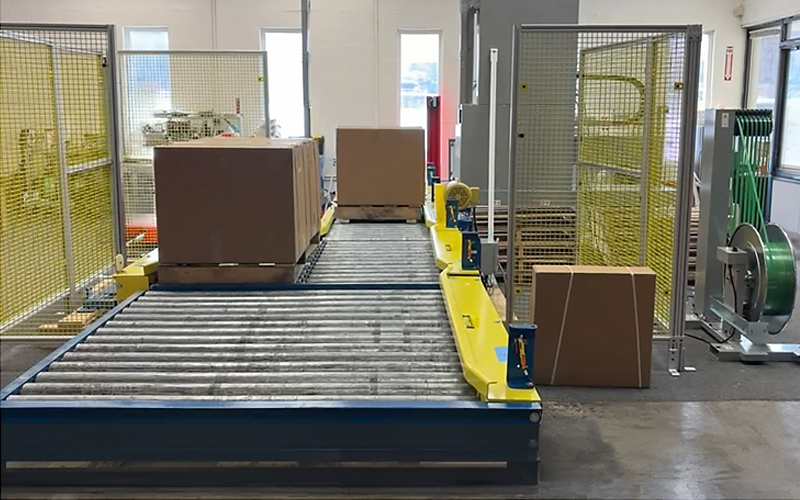
- Heavy-Duty Pallet Guides
- Forklift Backstops and Guards
- Adjustable End Stops
- End Stops with Fork Cutouts
Each component was selected to address the demanding operating conditions, accommodate pallet variations, and support reliable material flow.
Selected conveyor sections incorporated freezer-duty, low-temperature lubrication and SuperLube grease for the bearings to help maintain dependable performance in the -20°F environment.
Alba also provided detailed 3D CAD models of its conveyor equipment, allowing AEC to incorporate the components directly into its pallet down-ender design. These models helped streamline system integration and enabled AEC to present a complete, accurate equipment layout during customer design reviews.
The ability to visualize the integrated system in three dimensions helped AEC address equipment placement, conveyor interfaces, and overall system configuration before installation.
The Results
The collaboration between Alba Manufacturing and AEC produced an application-specific conveyor design that addressed the demanding requirements of automated pallet handling in extreme cold.
The engineered solution provided several important advantages:
- Freezer-Ready Performance: Conveyor components and selected low-temperature lubricants were specified for operation in temperatures as low as -20°F.
- Heavy-Duty Load Handling: Equipment was designed to accommodate 2,500-pound palletized loads on both CHEP and GMA pallets.
- Improved Equipment Protection: Forklift guards, backstops, pallet guides, and adjustable stops addressed the demands of forklift interaction and pallet positioning.
- Seamless System Integration: Detailed 3D CAD models supported integration with AEC’s pallet down-ender and simplified customer design reviews.
- Long-Term Durability: Rugged construction and application-specific engineering addressed the mechanical demands of continuous industrial pallet handling.
By combining AEC’s expertise in cold storage automation with Alba’s heavy-duty conveyor engineering capabilities, the project delivered a coordinated equipment solution designed to support reliable operation in an exceptionally demanding environment.
The Alba Advantage
Extreme cold introduces challenges that conventional conveyor equipment is not always designed to handle. Successful freezer applications require more than temperature-rated components. They demand a thorough understanding of pallet characteristics, load handling, mechanical design, lubrication, equipment protection, and system integration.
This project demonstrates how Alba Manufacturing works with its integration partners to develop practical, durable conveyor solutions for specialized material handling applications.
When heavy loads, automated processes, and subzero temperatures come together, Alba delivers conveyor equipment engineered for the challenge.
Application Information
Product Information
- Pallet Size: 40″ x 48″ CHEP and GMA Pallets
- Maximum Load: 2,500 lb.
- Application: Palletized Load Movement into and Out of a Freezer Environment
- Operating Environment: -20°F Freezer Area
Conveyor Specifications
Two (2) Model 251160-3-DBS CDLR Conveyors
- 5’3″ long
- 52″ Effective Width
- 1 HP Super “E” Motors
- Freezer-duty Low-temperature Lubrication
- SuperLube Grease for Bearings
- RAL 9005 Jet Black Paint
- Safety Yellow Guards
Two (2) Model 251140-3.25 CDLR Conveyors
- 4’8″ Long
- 52″ Effective Width
- 1/2 HP Super “E” Motors
Two (2) Model TDST/TFT251160-4.5-3S Thru-Drive-Side and Thru-Frame Transfers
- One at 7’3-3/4″ Long
- One at 1’’2-1/4″ Long
- 52” Effective Width
- 1/2 HP Super “E” Motor for CDLR Conveyor
- 1 HP Super “E” Motor for Transfer Chains
Eight (8) Model 251160-4.5 CDLR Conveyors
- Seven at 4’10-1/2″ Long
- One at 7’1-1/2″ Long
- 52″ Effective Width
- 1/2 HP Super “E” Motors
Eight (8) Model 251140-3.25 CDLR Conveyors
- One at 4’8″ Long
- Five at 4’11-1/4″ Long
- One at 5’5-3/4″ Long
- One at 5’9″ Long
- 52″ Effective Width
- 1/2 HP Super “E” Motors
Six (6) Model TFT 251160-4.5-3S Thru-Frame Transfers
- Five at 4’10-1/2″ Long
- One at 6’0″ Long
- 52″ Effective Width
- 1/2 HP Super “E” Motor for CDLR Conveyor
- 1 HP Super “E” Motor for Transfer Chains
Value Added Features
- Freezer-duty Lubrication and Grease for Selected CDLR Conveyors
- Hydraulic Actuated Chain Transfers for Freezer Application
- Low-temperature Rated Conveyor Sections
- Heavy-duty Pallet Guides
- Adjustable End Stops
- Back Stops
- End Stops with Fork cutouts
- Forklift Guarding
- Solid Models to Support System Integration and Customer Design Review
About Us
Alba Manufacturing, established in 1973, engineers and designs heavy-duty roller conveyor systems. Our systems consist of chain driven live roller (CDLR), zero pressure accumulation, drag chain, gravity, lift and rotate, pallet stackers and dispensers, turntables, chain transfers and transfer cars. Our corporate office and manufacturing facility is located in Fairfield, Ohio, approximately 30 minutes north of Cincinnati, Ohio.
For more information regarding this application/solution, please contact us via phone at 866.252.2634; via web at www.albamfg.com or via email at RockSolidConveyor@albamfg.com.