Heavy-Duty Pallet Handling Solution Helps NSH USA Maximize Floor Space and Streamline Material Flow
The Challenge
NSH USA Corporation, a manufacturer of specialized machine tools and automation systems, needed a heavy-duty conveyor solution for two automated railway wheel set production facilities in North America.
Based in Albany, New York, NSH USA is part of the international NSH Group (NILES-SIMMONS-HEGENSCHEIDT), which supplies advanced machine tools and automation technology to the railway, automotive, aerospace, and other industrial markets.
The facilities, commonly known as “wheel shops,” are designed to inspect, repair, and rebuild worn railway wheel sets used by freight and transit operators.
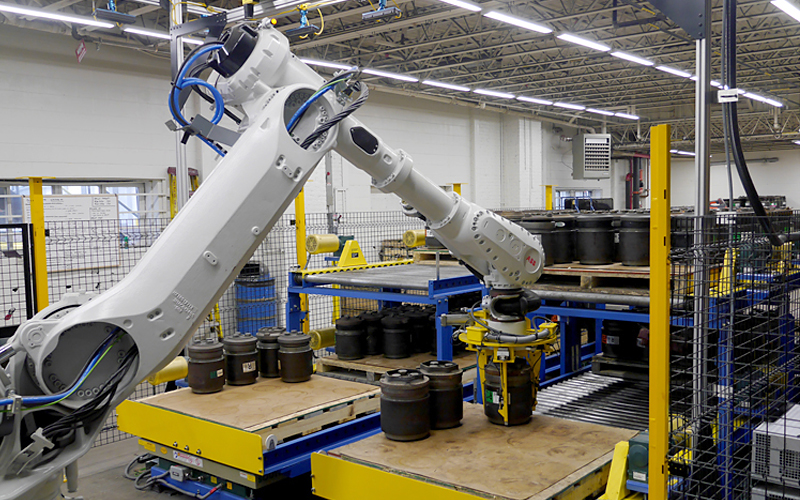
Each facility required a powered roller conveyor system capable of transporting palletized wheel set components into and out of automated repair cells. The system needed to handle heavy loads while minimizing the floor space required for inbound and outbound material movement.
The application presented several specific requirements:
- Pallet Size: 48″ wide x 48″ long, 4-way reverse GMA-style pallets
- Maximum Load Capacity: 2,000 pounds per pallet
- Pallet Orientation: Bottom boards positioned parallel to the conveyor rollers (hard-way orientation)
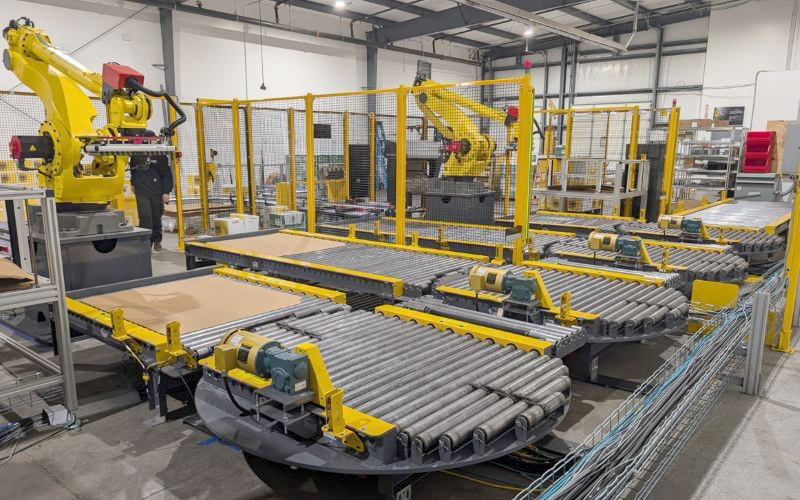
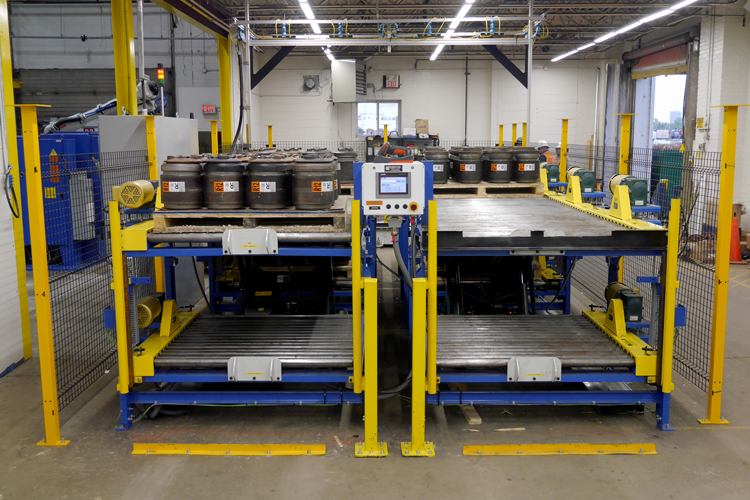
- Conveyor Configuration: Over/under powered roller conveyor system providing inbound and outbound transportation at two levels
- Operational Requirements: Reliable movement of heavy palletized components through an automated railway wheel set repair process
Given the weight of the components and the demands of the application, conveyor construction, durability, and dependable operation were critical considerations.
The Alba Solution
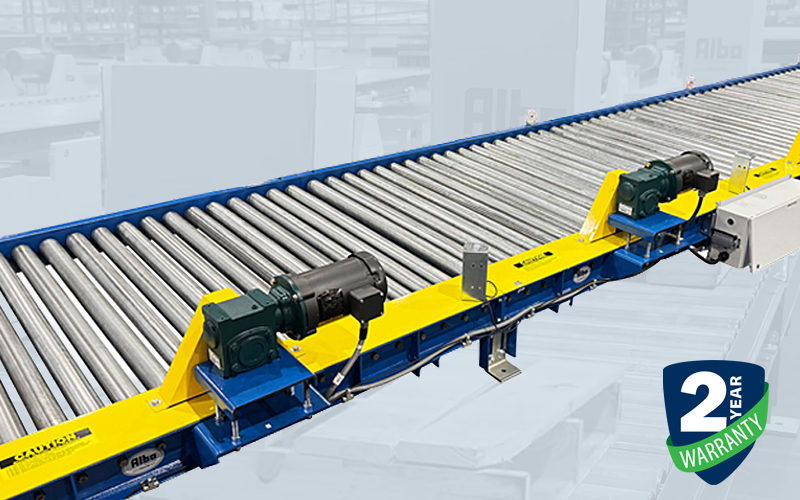
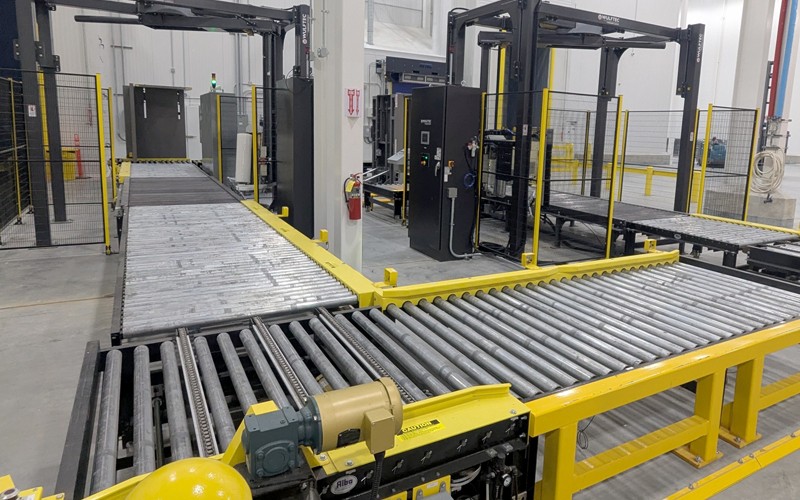
NSH USA partnered with Alba Manufacturing to provide a heavy-duty over/under powered roller conveyor system specifically suited to the application.
Alba’s reputation for rugged construction, proven conveyor designs, and dependable material handling equipment made it a strong fit for the project.
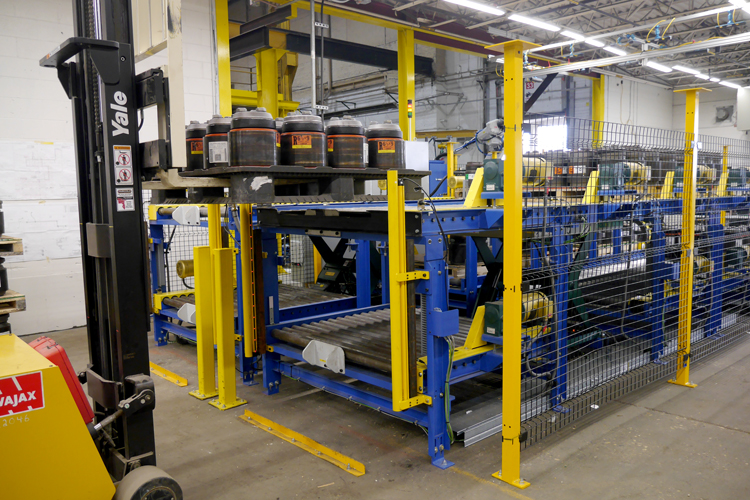
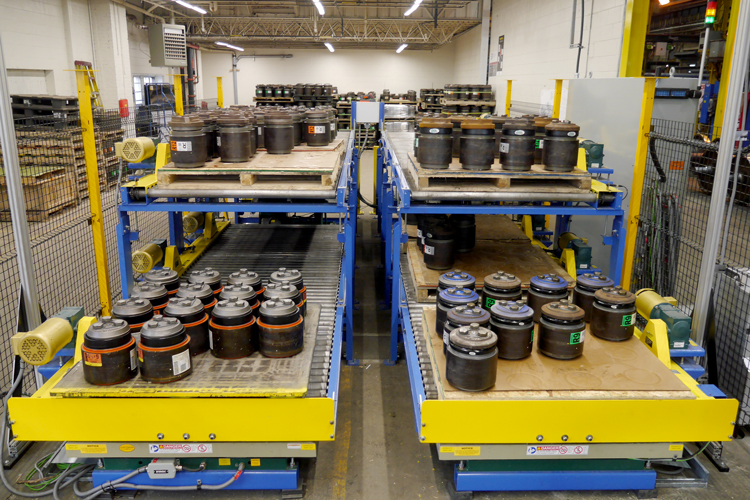
The over/under configuration allows palletized components to travel into and out of the repair cell at two separate elevations. Rather than requiring two independent conveyor lines positioned side by side, the system uses vertically arranged conveyor levels to reduce the overall footprint.
This design is particularly beneficial in automated manufacturing environments where floor space is valuable and equipment must be positioned to support an efficient production sequence.
Alba’s heavy-duty construction provides the strength necessary to support pallets weighing up to 2,000 pounds while accommodating the specified hard-way pallet orientation.
Supporting the Wheel Set Repair Process
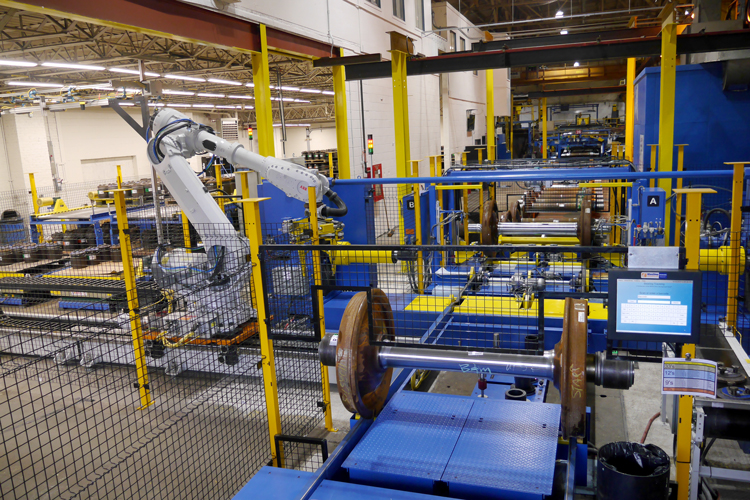
Within the automated wheel shops, NSH USA’s SIMMONS brand machines inspect and process railway wheel set components, including wheels, axles, and bearings.
Components are evaluated to determine whether they can be repaired or reclaimed. Those that are damaged or worn beyond repair are scrapped, while reusable components proceed through the appropriate machining and reconditioning operations.
Additional SIMMONS equipment performs machining and processing operations, including installing new wheels and bearings on reclaimed axles.
Throughout this process, components must move between processing stages reliably and efficiently.
Alba’s over/under conveyor system supports this movement by transporting palletized components into the repair cell and providing a separate level for outbound material handling.
Once processing is complete, the components can be conveyed out of the repair cell for subsequent handling and shipment.
The Results
At the time of the project report, NSH USA was manufacturing and testing the two automated railway wheel set production facilities incorporating Alba’s conveyor equipment.
The over/under conveyor design provides several important operational advantages:
- Reduced Floor Space Requirements: Vertically arranged inbound and outbound conveyor levels reduce the footprint compared with separate side-by-side conveyor lines.
- Heavy-Duty Load Handling: The system accommodates palletized components weighing up to 2,000 pounds.
- Improved Material Flow: Separate conveyor elevations support organized movement into and out of the automated repair cell.
- Application-Specific Design: The conveyor configuration accommodates the required pallet dimensions, orientation, and material handling sequence.
- Integration with Automated Equipment: The system is designed to work within NSH USA’s automated railway wheel set repair operations.
Together, these capabilities provide a practical conveyor solution for demanding railway maintenance and manufacturing applications.
Built for Demanding Industrial Applications
The NSH USA project demonstrates how an application-specific conveyor design can address multiple material handling challenges without unnecessarily increasing equipment complexity or floor space requirements.
By combining heavy-duty powered roller conveyor construction with an efficient over/under configuration, Alba Manufacturing provided NSH USA with a solution designed to support reliable material flow in a demanding automated production environment.
Need a heavy-duty pallet handling solution for your operation?
Alba Manufacturing designs and builds rugged conveyor equipment for challenging industrial applications. From specialized conveyor configurations to complete pallet handling solutions, Alba works with system integrators and equipment manufacturers to deliver dependable, application-specific equipment.
Conveyor/Product Specifications
- Eight (8) 251140-3.25 CDLR Over/Under Conveyors x 4’11-1/4″ long, 52” Effective Width, 40 FPM, 1 HP Baldor Super “E” Motors and Dodge Tigear II Gear Reducers, High Side Drives, 23″ Top of Roller (Lower Level), 55″ Top of Roller (Upper Level)
- Sixteen (16) Special common two-tiered, heavy duty supports for 23″ (bottom level) and 55″ (top level) top of roller elevations, fabricated from 5″ @ 6.7# channel legs, channel welded cross ties, adjustable foot. Each conveyor includes two (2) supports and one (1) set of knee bracing per support
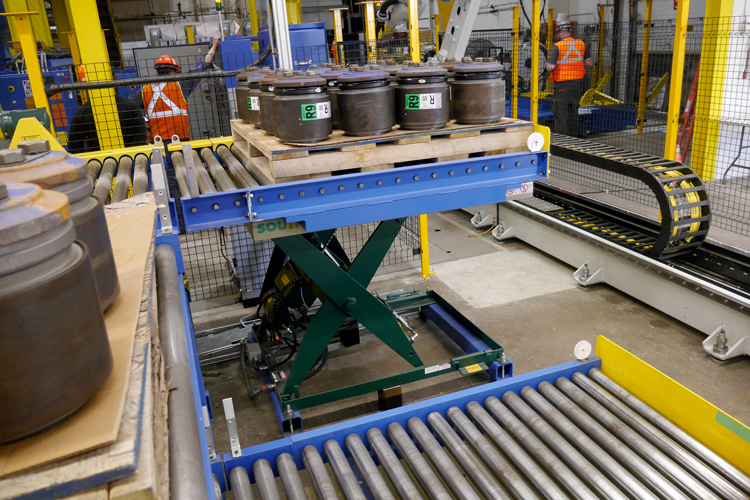
- Two (2) 251140-3.25 Chain Driven Live Roller Conveyors with Scissor Lift Base x 4’11-1/4″ long, 52″ Effective Width, 40 FPM, 1 HP Baldor Super “E” Motors and Dodge Tigear II Gear Reducers, High Side Drives, 23″ Top of Roller (Lowered), 55″ Top of Chain (Raised). Conveyor mounted to a scissor lift by Alba.
Value Added Features
- Includes an external proximity stand x 60″ tall with an upper proximity and a lower proximity and a slow-down proximity just above the lower switch. Alba mounted a flag on the side of the lift platform for location detection.
- Fixed End Stop with Fork Cutouts
- Pre-Assembled Conveyors with 2-Tiered Supports Mounted Prior to Shipment
About Us
Alba Manufacturing, established in 1973, engineers and designs heavy-duty roller conveyor systems. Our systems consist of chain driven live roller (CDLR), zero pressure accumulation, drag chain, gravity, lift and rotate, pallet stackers and dispensers, turntables, chain transfers and transfer cars. Our corporate office and manufacturing facility is located in Fairfield, Ohio, approximately 30 minutes north of Cincinnati, Ohio.
For more information regarding this application/solution, please contact us via phone at 866.252.2634; via web at www.albamfg.com or via email at RockSolidConveyor@albamfg.com.
Photo Credit: NSH USA Corporation